DLT-5830
PVC Fabric for Equipment Bag Panels
A PVC and woven polyester composite for equipment bags and reusable industrial packaging.
- Weight
- 500gsm
- Width
- 1.05–3.2 m
Product images
TECHNICAL DATASHEET
| Structure: | PVC / Polyester base fabric / PVC |
|---|---|
| Base fabric: | 500D × 500D / 18 × 17 threads/inch |
| Weight: | 500gsm |
| Width: | 1.05–3.2 m |
| Customization options: | Color / Thickness / Roll width / Flame retardancy / Environmental compliance / Anti-static / Anti-mildew / Antibacterial |
| Tensile strength: | 1283/1120N/5cm |
| Tearing strength: | 270/230N/5cm |
| Peeling off strength: | 65N/5cm |
| Reference test methods: | Tensile: ISO 1421; tear: DIN 53363; coating adhesion: DIN 53357. |
| Fabrication methods: | Hot-air welding / High-frequency (HF) welding / Sewing |
| Suitable temperature: | −30 to +70 °C |
| Flex resistance: | >50,000 cycles — DIN 53359 A |
| Package: | Paper tube + Kraft paper |
| Meter per roll: | 50-500m |
APPLICATIONS:
Product Features
- AntistaticOptionalAvailable as an optional configuration. Helps manage electrostatic charge build-up in the fabric, giving manufacturers a material option for assemblies with specified static-control requirements.
- Flame retardantOptionalAvailable as an optional configuration. A flame-retardant formulation for fabricators supplying projects with defined fire-behaviour requirements. Select the grade around the test method required for the finished application.
- Mildew resistantOptionalAvailable as an optional configuration. A mildew-resistant formulation helps address surface growth in damp or humid service conditions and during storage between uses.
Understanding the Reinforcement
A 500D yarn designation describes yarn linear mass, while the 18 × 17 count describes how frequently yarns occur in the woven base. They answer different questions about the reinforcement. In DLT-5830, that base sits between PVC faces, so the outside appearance does not reveal every detail of the textile. Compare tensile, tear and adhesion data alongside the construction when reviewing a bag material.
Planning the Joints
Hot-air welding, high-frequency welding and sewing are listed conversion options for DLT-5830. The best joint depends on the bag design and equipment available to the converter. Include folded edges, strap patches and closures in a trial assembly. Where the bag must limit water entry, review the complete seam and closure arrangement as well as the PVC sheet itself; a coated face does not seal every assembled opening.
Application requirements — Waterproof Bags
Specify the finished size, contents, carried load, closure design and the way handles or straps attach. Review tear propagation, abrasion, coating adhesion and the reinforcement around seams and attachment points. Agree the intended water-exposure level and a finished-bag test method rather than inferring protection from the sheet material alone.
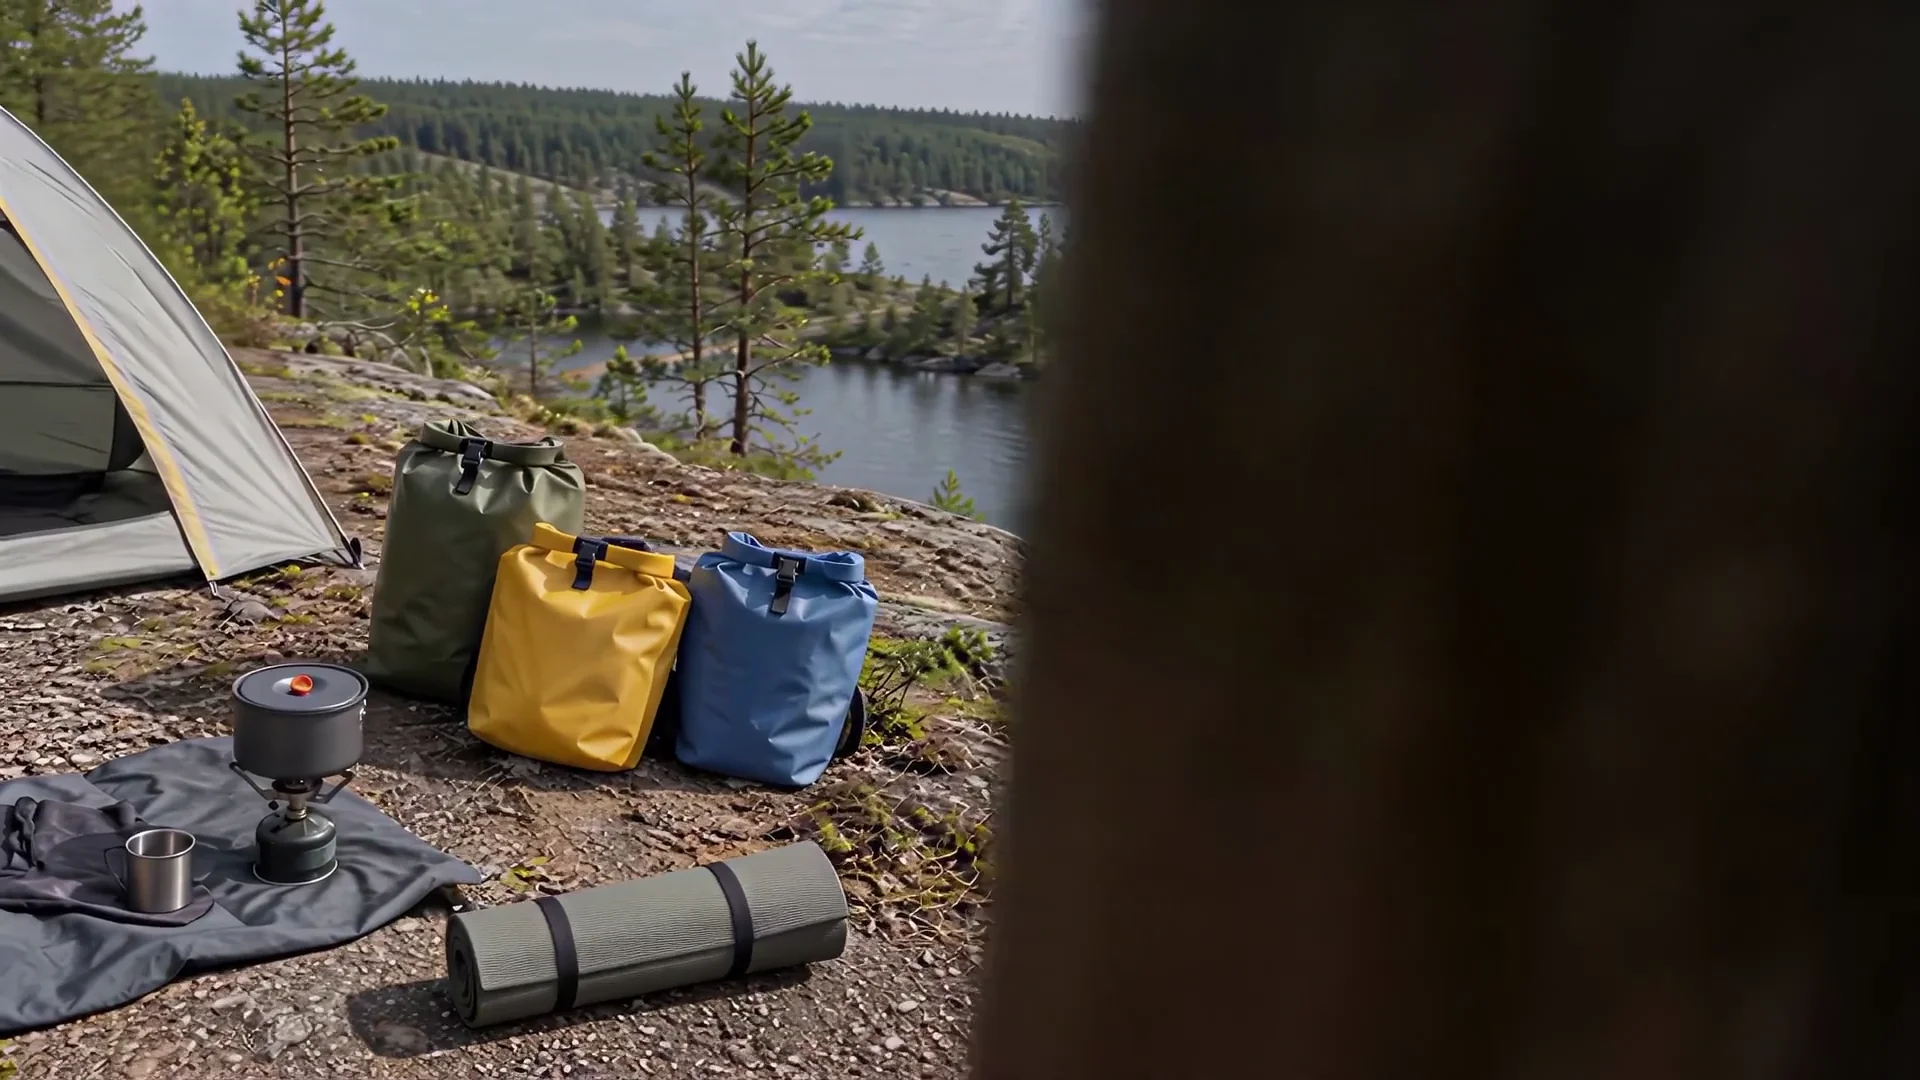
Finished Roll-Top Dry-Bag Configurations
These dimensions describe closed roll-top bags. Leave sufficient fabric above the usable compartment to form the closure.
| Specification | Configuration |
|---|---|
| 10 L Example | 34 cm closed height × 19 cm diameter |
| 22 L Example | 52 cm closed height × 22 cm diameter |
| 35 L Example | 60 cm closed height × 27.5 cm diameter |
| Top Closure | Roll top with a stiffener strip and side-release buckle |
| Closure Allowance | The example sizes use 3–4 rolls; the open bag is approximately 20 cm taller |
| Base Construction | Reinforced bottom panel with a separate bottom holding loop |
| Attachment Points | D-rings and buckle connections on reinforced attachment areas |
| Water-Exposure Check | Confirm the finished closure and seam test; a roll-top bag is not automatically suitable for immersion |
Construction Details
Roll-Top Opening
The stiffener helps form an even roll across the opening. Usable volume is measured with the required closure rolls already made.
Bottom Panel And Loop
The base and its joint carry repeated packing contact. A bottom loop can assist holding or securing the bag, with its attachment assessed separately from the body fabric.
Material Insights 3 videos
Heavier Isn't Always Stronger: Choosing PVC Tarpaulin
Material Guide
Discuss the application.
For PVC fabric bag panels, share the cutting pattern, joining method and attachment details for sample review.
PVC Faces and a Woven Core for Equipment Bags
DLT-5830 combines a woven polyester base with PVC on both faces. Its 500D × 500D yarn and 18 × 17 threads per inch describe the reinforcement inside the sheet. The polyester provides a textile framework, while the PVC faces form the exposed material that the bag maker cuts, joins and handles. The listed weight is 500gsm for the complete composite, rather than the weight of its polyester core alone.
The layer description does not identify a particular coating or lamination route. It does, however, identify hot-air welding, high-frequency welding and sewing as fabrication methods. These describe ways of making the bag after the roll material has been produced. A welded joint joins compatible PVC surfaces; a sewn joint makes a line of needle penetrations and may require a separate sealing detail where water entry matters. Handles, buckles and load-bearing straps need their own attachment design.
The table lists tensile values of 1283/1120N per 5cm and an adhesion value of 65N per 5cm. These measurements describe different parts of the composite: tension acts through the sheet, while adhesion concerns the bond between its layers. When selecting equipment bag panels, consider the fabric where corners fold, where contents rub and where reinforcement patches overlap. A sample bag section gives a more useful view of seam bulk and handling than a flat colour swatch alone. The available width is 1.05–3.2m, with roll length selected within the listed 50–500m range.